Quality & Safety
Quality is not an inspection. It is a process.
A final check tells you whether one belt is acceptable. It tells you almost nothing about the next thousand. So the controls sit inside the process instead of at the end of it.
Controls / 01
Where quality is actually decided
Nine control points, ordered roughly as a part encounters them. Each exists because a specific class of defect becomes expensive or invisible if it gets past.
01
Material consistency
Webbing is the load path, so variation in width, thickness or weave changes how the finished belt elongates. Incoming webbing is checked against the specification before it is committed, because once it is cut and assembled the variation is built in.
02
Component quality
Hardware is checked dimensionally and visually on arrival. A latch plate with a slot a fraction too wide will still take webbing and will still latch — and will let the webbing move under load, which is precisely the failure that is hardest to see.
03
Assembly accuracy
Hardware position and orientation are verified against the specification, not against the previous unit. Copying the last one is how a small error becomes a whole batch.
04
Dimensional verification
Overall length and sub-lengths are measured, because those dimensions decide where the latch plate and buckle meet on the occupant and whether the belt reaches its anchorage at all.
05
Functional inspection
The assembly is operated: latch plate inserted to confirm positive engagement, button pressed to confirm clean release, and where a retractor is fitted, webbing drawn out and returned to confirm smooth payout and full retraction.
06
Visual inspection
Webbing surface, cut ends, hardware finish and securing points are examined. This catches what measurement misses — abrasion, a burr, contamination, a scuffed part that is dimensionally perfect and cosmetically unacceptable.
07
Process control
One documented method per part, held for the whole run, with stages completed in sequence. Where a method could be read two ways it gets rewritten, because ambiguity is what produces drift between operators and between shifts.
08
Documentation & traceability
Checks are recorded against the batch, so a question about a delivery can be answered from records rather than recollection. The level of traceability required varies by project and is agreed as part of the specification.
09
Continuous improvement
When something is found — at inspection or after delivery — the useful question is which control should have caught it. Fixing the unit is housekeeping; moving or adding the control is the actual correction.
Background / 02
Understanding automotive restraint systems
A short, plain explanation of how a seat belt does its job — useful context when specifying one.
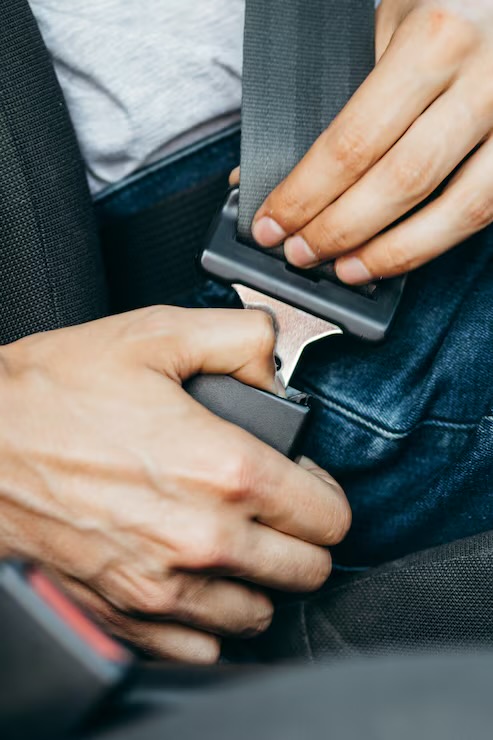
Fig. 01Latch plate entering the buckle throat
Why seat belts matter
In a sudden stop, an unrestrained occupant keeps moving at the speed the vehicle was travelling until something stops them. A seat belt makes that something the belt itself — spread across the strongest parts of the body, over a longer distance, and in a direction the body can tolerate.
How the restraint works
The webbing holds the occupant against the seat and transfers load into the vehicle structure through the anchorages. Because the webbing is woven rather than rigid, it elongates in a controlled way, which stretches the deceleration over more time and reduces the peak force involved. Everything else in the assembly exists to make sure the webbing is in the right place, at the right length, when that happens.
What each part contributes
| Part | Role |
|---|---|
| Webbing | Carries the load and spreads it across the pelvis and rib cage; elongates in a controlled way. |
| Retractor | Stores webbing under light tension, pays it out as the occupant moves, locks when payout must stop. |
| Buckle | Accepts and holds the latch plate with a positive engagement; releases cleanly on demand. |
| Latch plate | Connects the webbing to the buckle and divides the belt into its shoulder and lap sections. |
| D-ring / height adjuster | Sets the angle the shoulder belt crosses the torso, so it clears the neck and sits on the shoulder. |
| Anchorages | Transfer load from the belt into the vehicle structure. |
Why correct assembly matters
Every one of those parts can be individually correct and the assembly still be wrong — webbing routed the wrong side of a D-ring, hardware fitted upside down, a length that puts the latch plate out of reach. Correct assembly is not a finishing touch; it is the difference between a load path that works and one that does not.
Never modify or bypass a restraint system
Seat belts, anchorages and their fixings should only be installed, replaced or adjusted by a competent person, using parts specified for the vehicle and to the vehicle manufacturer's requirements. Do not modify, defeat or bypass any part of a restraint system, and replace a belt that has been worn in a collision or shows damage to the webbing, hardware or buckle.
Standards / 03
How standards and documentation are handled
Restraint systems are regulated in every major vehicle market. Which framework applies depends on the vehicle, the seating position and where the vehicle will be sold — so this is settled per project rather than claimed in general.
Requirements come from the vehicle
The applicable standard is set by the vehicle programme and the market it is homologated for, not by the component supplier. We work to the requirement the buyer is obliged to meet.
Confirmed in writing, per enquiry
Applicable standards, test requirements and the documentation that has to accompany the parts are confirmed in writing against a specific product and market before anything is manufactured.
No certification claims on this site
We do not publish approval numbers, certificate references or test results as marketing. Where those are relevant, they are provided directly and can be verified.
Type approval is a separate activity
Regulatory type-approval and destructive testing are governed by the applicable standard and are distinct from the production checks described above.
Records follow the batch
Inspection results are recorded against the batch so a later query can be answered with evidence. The depth of traceability is agreed as part of the specification.
Changes are raised, not absorbed
If a component or method has to change mid-programme, that is a conversation with the buyer — never a silent substitution inside an approved specification.
Enquiries
Need to know what documentation we can provide?
Tell us the market, the vehicle and the standard you are working to. We will confirm in writing what applies and what we can supply against it.